Showing posts with label templates. Show all posts

Sunday, June 3, 2012

AMH-12 Core

As mentioned in my last post, I am making the cores for this years skis out of aspen, poplar, and oak. A core set of wood is shown below.


 Similar to years past, I am using what I call a pre-tensioned core design.  Rather than laminating thin strips of wood into a rectangle and then cutting the shape out of it, I cut two inner core members to a curve which allows for uniform wood strips in the center and on the sides of the core. Uniform strips on the ski edge  allow for even edge pressure.

The first step is to rip the core members to the predifined widths.  The three oak stiffeners are 5 mm wide.

Next, the shaped core members can be cut using the core member template.

Once this is done, the core members are sanded and can be glued together. A single core set is shown below consisting of 11 pieces.


This year I applied glue with a roller which improved the process over past years.


Once glued, a planer is used to create a smooth surface on both sides of the ski and to create the maximum thickness of 12 mm (binding platform).


The core template is then used to cut the shape of the tip and tail into the ski.  A jig saw works well for this.


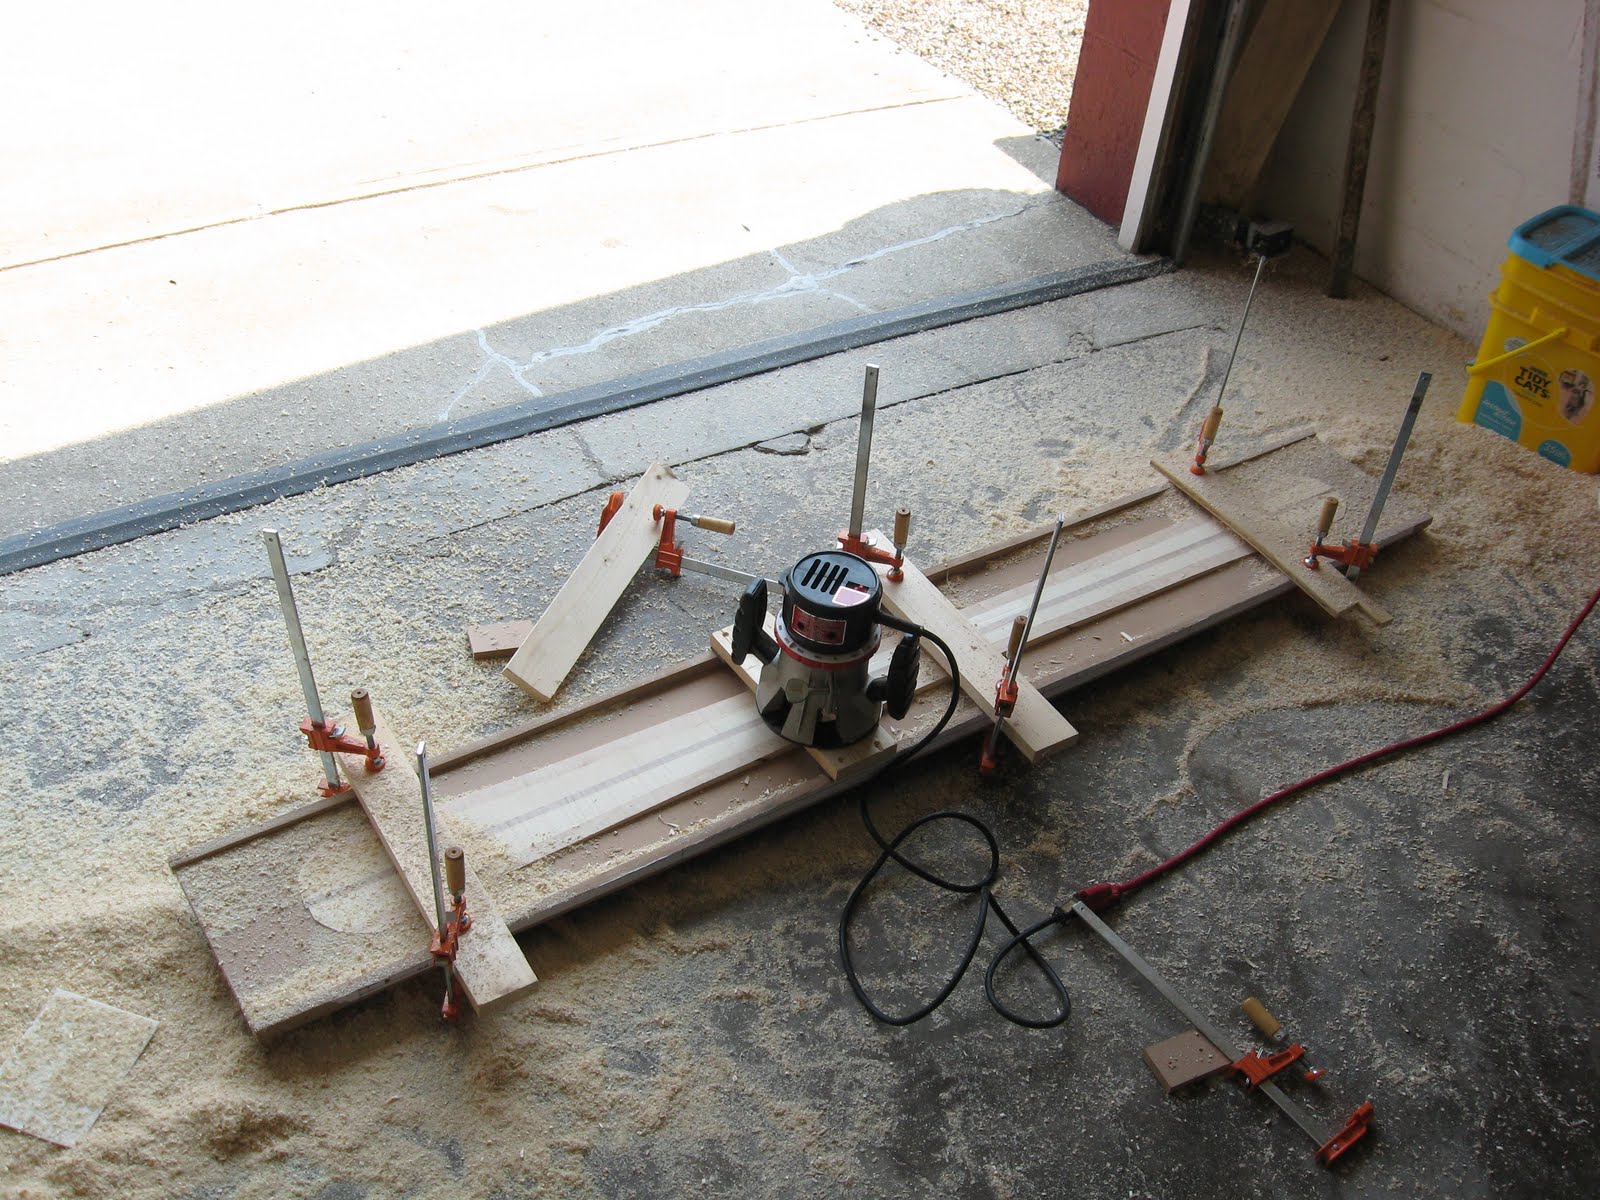
The next step is to set up the ski profiling jig and cut the ski thickness profile with a router.


 Once profiling is complete the core is again sanded.  Once sanded, the core is complete and ready for layup.

Friday, April 27, 2012

AMH-12

RECAP

The skis I made last year seem to have done well.  My brother has spent time skiing the Panjshirs at Crystal Mountain in the state of Washington.  The Arlias have seen east and west coast skiing and have performed well.  A pair of the Arlias even survive falling from the roof of a car onto the pavement at high speed. ( http://mwallworkrn.blogspot.com/2012_02_01_archive.html ).


I continued to use my Goliaths in the backyard and took the tomahawks to the slopes.  To date none of the skis I have made have failed and only a single Goliath V1 edge has torn out (I have corrected this problem).

2012

This year I decided to make only a single pair of skis. I want these skis to be good for east coast skiing, where I live, but also have the ability to take on big mountain snow. Additionally, I wanted the ski to be relatively light to take on backcountry trips. I have temporarily named the ski the All-Mountain Holuta (AMH-12).

The ski dimensions are 127-88-109 and 186 cm long.  Additionally, the ski has tip and tail rocker, camber, and reverse side cut at the tip and tail. The rocker will allow for easier powder skiing while the camber will allow for good edge grip on hard-pack. The reverse side cut at the tip and tail shortens the turning radius of the ski from ~21m to 17.7 m.  This will allow for quicker turning despite the length of the ski.  The reverse side cut will also lighten the ski and allow for smoother maneuverability in deep snow.  The ski was lengthened over past years (186 vs 181 cm) since the rocker shortens the contact length of the ski.  Adding a few centimeters to the length re-lengthens the contact length.  The final design is below:


In order to make the skis light, I am using Aspen, Poplar and Oak in the core.  Several 5mm strips of oak spread through the core serve to provide ample stiffness to the ski while filling the gaps with aspen and poplar lightens the ski.  Oak is not frequently used in skis, and I'm not entirely sure why.  It is a little expensive but it is very hard and stiff.  Oak is also stronger than the majority of commercially available woods.  The hardness wears out tools more quickly which may be why it's not used commercially.  I am also planning to add two oak rails to the top of each ski; this rail will significantly improve stiffness and edge grip. A preview of the core is below:


I have also started making the templates.  Similar to last year, I have three templates: a base, rough core, and core member template; the use of these templates will be explained later.  To make the templates, I had the designs printed full size and then used spray glue to attach them to high density fiberboard that I purchased.


The templates are then cut out and are ready to shape the ski.

Sunday, December 25, 2011

Post Job Assessment

After I finished the skis I decided that some stiffness testing was in order.  The stiffness of a ski is critical to its performance.  A backcountry or powder ski needs to be lighter and can be softer.  The soft snow is more forgiving and high speeds are not typically achieved.  An east coast carving ski needs to be relatively stiff to hold an edge at high speeds and avoid vibration.  To test the ski stiffness I placed weights on the ski and measured the deflection.  After searching my house for weights I only found two 5 lb weights.  Since a gallon of water weighs approximately 8 lbs, I filled a bucket up with two gallons to get an additional 16 lbs.

I tested all the skis that I have to get a good comparison.  The goal with the skis this year was to design them so that they would be stiffer that the first generation Goliaths and softer than the second generation Goliaths and Tomahawks. This goal was achieved.  In order off stiffness, here is how my skis rank up from stiffest to softest.
  1. Tomahawk
  2. Arlia (M)
  3. Arlia (R)
  4. Panjshir
  5. Elan Silver Magic
  6. Blizzard Titan
  7. K2 Kung Fuja
  8. Goliath V1
The graph below shows the test results when 5, 10, and 26 lbs was applied to each ski.  Note that I tested the Arlia and Panjshir prior to attaching the second layer of fiberglass and topsheet; these results are noted by a (PC) after the name.


The calculations that I performed prior to building the skis are summarized in the table below.  These calculations did not take into account the stiffening properties of the epoxy.  The test results show that the epoxy has an average 4.18 stiffening factor for non-metal skis and around 2.4 for skis with metal built into the core.  The skis I built with metal rods in the core were very stiff and therefore the epoxy had less of an effect on the stiffness.  Since I don't have a pair of the second generation Goliaths I could not test the stiffness (these skis belong to my brother).
Overall the skis turned out as I expected and have a stiffness within the range that I had hoped for.  The following is a summary of what I have learned this season:
  1. Rather than packing tape, use contact paper to protect the base and top sheet as the application and removal would be easier.
  2. The cost of printing out full size templates is worth while.  In the past I printed out the templates on 8.5 x 11 paper and taped the sheets together.  This worked, but the skis were never quite straight.
  3. Assuming a mold springback of 15 mm is safe.  The Arlia mold was designed with a 30 mm camber and came out at 15 mm, as planned.
  4. Paper is a good medium for appling graphics (acrylic paint) and when soaked in epoxy becomes 70-90% transparent.  Cotton cloth still works well for opaque solid colors.  Solid colored construction paper may work well also.
  5. If a cap construction is used rather than a plastic sidewall, then the sides of the skis must be sealed to make sure the core is sealed after edge grinding.
  6. 120 grit sand paper / grinding wheel is appropriate for edge grinding.
  7. A course jig saw blade works best when trimming flashing off of the skis after pressing.
  8. Isospeed 4400 p-tex base material grinds more easily than Durasurf 4001 p-tex base material.  This is likely due to the Isospeed material being slightly harder than the Durasurf material.
  9. West Systems Epoxy, 150B Resin / 206B Slow hardener wets up easily and provides enough time for lay-up without hardening.  The pumps are worth buying to easily measure out the epoxy.
  10. Mounting edges on the ski mold effectively holds the base in place during pressing and simplifies the process.

Monday, September 5, 2011

Core

The core of the ski is what gives the ski its feel and strength.  Wood is the preferred material for the ski core because of the flexibility, light weight, strength, and snap/feel.  Other materials can be substituted for wood, such as foam or foam rubber and plastic.  Wood and foam are often used together to create the desired core properties.

I prefer a solid wood core; wood is more expensive than foam, but provides for a better feel in my opinion. There are also many varieties of wood that can be mixed to create any feel (maple, poplar, aspen, ash, balsa, etc.). The core is designed with several factors in mind: primarily weight and flexibility (noodle vs barn door feel).  There is a balance here which ski manufactures work hard to achieve.  My first year I used a core made from poplar and aspen; these cores made for a very light ski, but it was also very flexible: the noodle. My second year I used aspen and maple, but also integrated steel and aluminum rods, 3 ft and 5 ft respectively, into the core.  The core was also thicker; this resulted in a ski that was heavy and rigid: the barn door.  These ski both have their place - backcountry/powder vs hard crud.  Last years cores are shown below:

 A 1/8" groove was routed into the side of the core members to place the 3' stainless steel and 5' aluminum rods in the core.


This year I attempted to balance the two by using my knowledge of the past two years.  The core is made from aspen and maple, but is thinner than year two.  I also tried to use some engineering logic to come to a conclusion:


The first step in creating the core is to rough cut the stock material.  This is done using a table saw to rip the boards down their length.  Their width is determined based on the core plans I originally laid out on my templates.


The next step is to cut the curved core members using a pre-fabricated template.  The cores I design use three constant width members and two variable width members.  The constant width members made from maple and run along the edges and in the center of the ski.  The two variable width aspen members are placed in-between the maple members.  I used this design because the constant thickness maple members on the edges create a constant edges pressure.  Also, the core is pretentioned into place.  This pretentioning adds some built-in stress to the ski which will add to edge pressure.  Ski manufacturers will not use this method because it wastes too much material, but I think the properties it gives is worth the loss.  Some of the following pictures will show the members and the pretensioning.  The variable width core members are cut with a jigsaw.


The core members and pretensioning method can be seen in the following pictures:


Using this method, the ski profile does not have to be cut, but is clamped into place. The core members should be sanded to remove any unevenness and ensure that the glue will bond well.


The next step is to clamp and glue the core into place;  I use a standard water resistant wood glue.  Placing a piece of plastic down on your work surface prior to gluing will help to control excess glue.


The core template can then be used to cut the rough tip and tail shape.  This is not the final shape as the core and flashing are trimmed after the ski is pressed.  The template is larger than the final ski by 5mm on every side.


At this point the ski must be planed to size.  The wood used is 3/4" thick which is equivalent to 19 mm.  The ski must be planed to 12 mm; this is the maximum thickness of the ski.  Using the planer is one of my favorite operations because it always works fast and well.


Once planing is complete, the ski thickness must be profiled to size.  A linear profile was chosen for these skis which takes them from 12mm at the boot to 2 mm at the tip and tail.  This is accomplished using the profiling jig that was created earlier.  A router is moved across the ski on a slide which is moved up and down the rail.


 A rapid material removal router bit works best.  It should create a flat cut.


 A slider is used to guide the router along the profiling jig rails.


The following video is played at 12X speed and demonstrates the profiling process.  It takes approximately 20-25 minutes per ski.


The cores are then sanded to remove any unevenness.  Once finished, the cores are ready to be pressed.