Showing posts with label Router. Show all posts

Sunday, November 23, 2014

All Mountain Radacoski (AMR-14)

It's been a busy year, but I am currently making a pair of skis for a friend, Matt Radacosky.  I am also in the process of building a new ski press from steel, but will post about that later. This year I am making a pair of eastern all mountain/freeride skis similar to the Aftermath of last year, but wider.  The aftermath is 127-88-109, 53% of the ski is in front of center, and has a turn radius of 17.7m.  The AMR-14 is 128-100-118, 51% of the ski is in front of center, and has a turn radius of 19.9m.  You can see the difference between the skis below.


I am also going with a sidewall design this year rather than the cap design.  I expect the ski to be a little heavier, but should be more responsive in turns. One change I am making this year is using a basalt fiber instead of fiberglass - basalt is made from igneous rock. Here is some info about basalt:

Basalt fiber is a material made from extremely fine fibers of basalt, which is composed of the minerals plagioclase, pyroxene, and olivine. It is similar to carbon fiber and fiberglass, having better physicomechanical properties than fiberglass, but being significantly cheaper than carbon fiber. (http://en.wikipedia.org/wiki/Basalt_fiber)

...the basalt/epoxy sample's strength tested 13.7 percent higher than that of the E-glass sample and exhibited 17.5 percent greater stiffness, although the basalt sample was 3.6 percent heavier than the E-glass sample. Additionally, basalt fibers are naturally resistant to ultraviolet (UV) and high-energy electromagnetic radiation, maintain their properties in cold temperatures, and provides better acid resistance. (http://www.compositesworld.com/articles/basalt-fibers-alternative-to-glass)

 Relative tensile strengths (breaking strength) are listed below:

Steel                  73000 psi  (0.50 GPa)
E-glass            500000 psi  (3.45 GPa)
Basalt              600000 psi  (4.15 GPa)
Carbon Fiber   725000 psi  (5.00 GPa)


After some extensive searching, I found some quad-axial basalt fabric from a company in Germany -iXperial (http://www.ixperial.net/). I highly recommend them; this shipment was fast and the customer service was excellent. Most fiberglass in skis is tri-axial, meaning that it is layered along three axes.  The basalt fiber I ordered is layerd on four.  The basalt will be visible through the topsheet and graphics layer.


This year I purchased a new 2.5HP router and a 6 Amp jig saw.  If I could afford a large bandsaw I'd have one.  The extra power in these tools over my past tools makes a big difference in cutting time and surface finish.  The core of the ski is nearly identical to the Aftermath, but substitutes pine for the cedar.  It still uses 3 oak stringers, 5mm wide, along with Aspen and Poplar. Photos of the core in process are below.


The base material is simlilar to last year and is a 4001 grade sintered P-Tex. This year I was able to get the base template and core member template printed on the same sheet, which saved some time and money.  The base in process is below.


I did run into a problem this year; after I cut out the base and superglued on the edges, I realized that one base had warped out of shape.  I have speculated that it had something to do with internal stresses in the base material.  When the material was cut, the stresses were relieved and it warped.  It's common in steel and I have seen it in plastic tubing before.  I had to re-order the base material and try again.  This time I cut out the base roughly at first, leaving about 1 inch to the template.  I then took a second pass using the template and it turned out fine.

I am returning to the sidewall design again this year.  The following pictures illustrate attaching the sidewalls to the core, planing the core, and profiling the core.


My friends Matt and Shane;  Shane is determined to make skis with me for a living; I forced them both to wear hearing protection.


Once the skis were profiled, I used my belt sander and 50 grit sand paper to smooth out the surface after routing. One thing I was worried about, after my last experience with sidewalls, was getting the sidewall to stick to the epoxy.  Ideally, the plastic surface would be very rough with a surface finish that looks like that of the base material.  The 50 grit belt seemed to do the job quite well as shown below.  The surface looks like it does when it is abraded at the factory. This will give the epoxy "hairs" to grab onto as it forms a mechanical bond.  A lesser grit would produce a cleaner looking surface, but would not bond as well.


The next step is to finish the graphics layer, prep the top sheet and basalt layers, and press the skis.
 
Here is a preview of the new ski press.


Saturday, August 17, 2013

The Core

It has been about 4 months since I have done any work on my skis because our second daughter was born in April. She is a wonderful blessing to our family and worth suspending ski building operations for.  I am excited for the day when my children out-ski me for the first time.

"Exactly one day in your life your kid will ski as good as you do. The next day, he'll ski better than you."
-Warren Miller

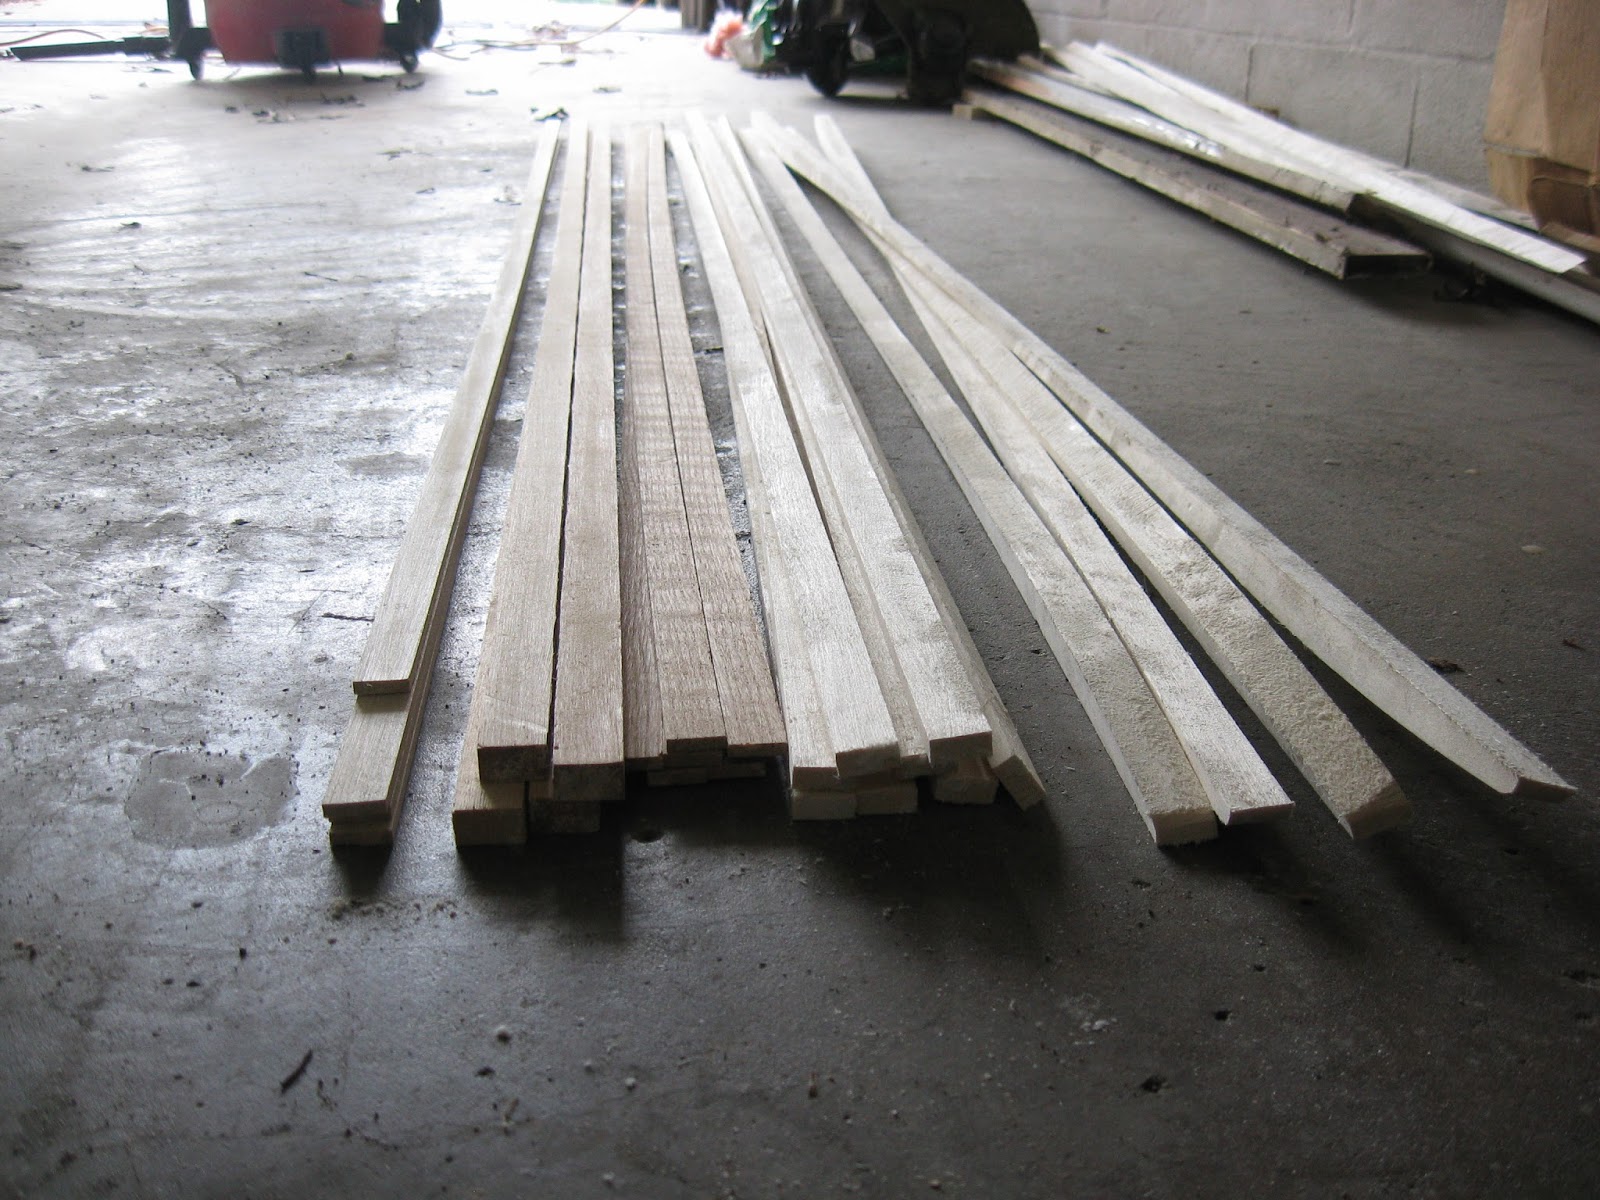
The Aftermath 2 core is nearly identical to the Aftermath gen 1 core except that cedar was substituted for several aspen members to lighten the core.  Also, the oak rails will not be included with this model since they provide too much stiffness.  This will be my lightest core ever.  The core is comprised of 13 members as shown below:


This is my first year using cedar and I had to find a piece with no knots, but this turned out to be pretty easy; all the wood was purchased at Lowe's.  Cutting the core members is fairly straightforward with a table saw - just watch your fingers with the 5mm wide pieces.


Once done, I used my core member template to cut the two curved aspen members for each ski.  Then I used a 50 grit belt on my belt sander to finish the cuts.  Clamping the boards together allows the sander to ride perpendicular to the top of the member.  It also ensures all the members are identical.
 
Aspen Curved

 Aspen Straight 
 
 Oak
 
 Cedar
 
 Poplar


Once the sanding was complete, all the wood was wiped clean with a damp cloth.  Wood glue, clamps, and a paint roller were used to join the core members.


The core is in its final stages now and can be planed down from 19mm to 12mm thick.


Next the core template is used to round the tip and tail of the core blank.

 
The ski is then clamped into the profiling jig and a router is used to machine the core blank to thickness.  The tip and tail are machined from 12mm to 2mm.


Another sanding, this time with 80 grit sandpaper, is needed to smooth out the surface created by the router.  The core is now ready for layup.


Monday, September 5, 2011

Core

The core of the ski is what gives the ski its feel and strength.  Wood is the preferred material for the ski core because of the flexibility, light weight, strength, and snap/feel.  Other materials can be substituted for wood, such as foam or foam rubber and plastic.  Wood and foam are often used together to create the desired core properties.

I prefer a solid wood core; wood is more expensive than foam, but provides for a better feel in my opinion. There are also many varieties of wood that can be mixed to create any feel (maple, poplar, aspen, ash, balsa, etc.). The core is designed with several factors in mind: primarily weight and flexibility (noodle vs barn door feel).  There is a balance here which ski manufactures work hard to achieve.  My first year I used a core made from poplar and aspen; these cores made for a very light ski, but it was also very flexible: the noodle. My second year I used aspen and maple, but also integrated steel and aluminum rods, 3 ft and 5 ft respectively, into the core.  The core was also thicker; this resulted in a ski that was heavy and rigid: the barn door.  These ski both have their place - backcountry/powder vs hard crud.  Last years cores are shown below:

 A 1/8" groove was routed into the side of the core members to place the 3' stainless steel and 5' aluminum rods in the core.


This year I attempted to balance the two by using my knowledge of the past two years.  The core is made from aspen and maple, but is thinner than year two.  I also tried to use some engineering logic to come to a conclusion:


The first step in creating the core is to rough cut the stock material.  This is done using a table saw to rip the boards down their length.  Their width is determined based on the core plans I originally laid out on my templates.


The next step is to cut the curved core members using a pre-fabricated template.  The cores I design use three constant width members and two variable width members.  The constant width members made from maple and run along the edges and in the center of the ski.  The two variable width aspen members are placed in-between the maple members.  I used this design because the constant thickness maple members on the edges create a constant edges pressure.  Also, the core is pretentioned into place.  This pretentioning adds some built-in stress to the ski which will add to edge pressure.  Ski manufacturers will not use this method because it wastes too much material, but I think the properties it gives is worth the loss.  Some of the following pictures will show the members and the pretensioning.  The variable width core members are cut with a jigsaw.


The core members and pretensioning method can be seen in the following pictures:


Using this method, the ski profile does not have to be cut, but is clamped into place. The core members should be sanded to remove any unevenness and ensure that the glue will bond well.


The next step is to clamp and glue the core into place;  I use a standard water resistant wood glue.  Placing a piece of plastic down on your work surface prior to gluing will help to control excess glue.


The core template can then be used to cut the rough tip and tail shape.  This is not the final shape as the core and flashing are trimmed after the ski is pressed.  The template is larger than the final ski by 5mm on every side.


At this point the ski must be planed to size.  The wood used is 3/4" thick which is equivalent to 19 mm.  The ski must be planed to 12 mm; this is the maximum thickness of the ski.  Using the planer is one of my favorite operations because it always works fast and well.


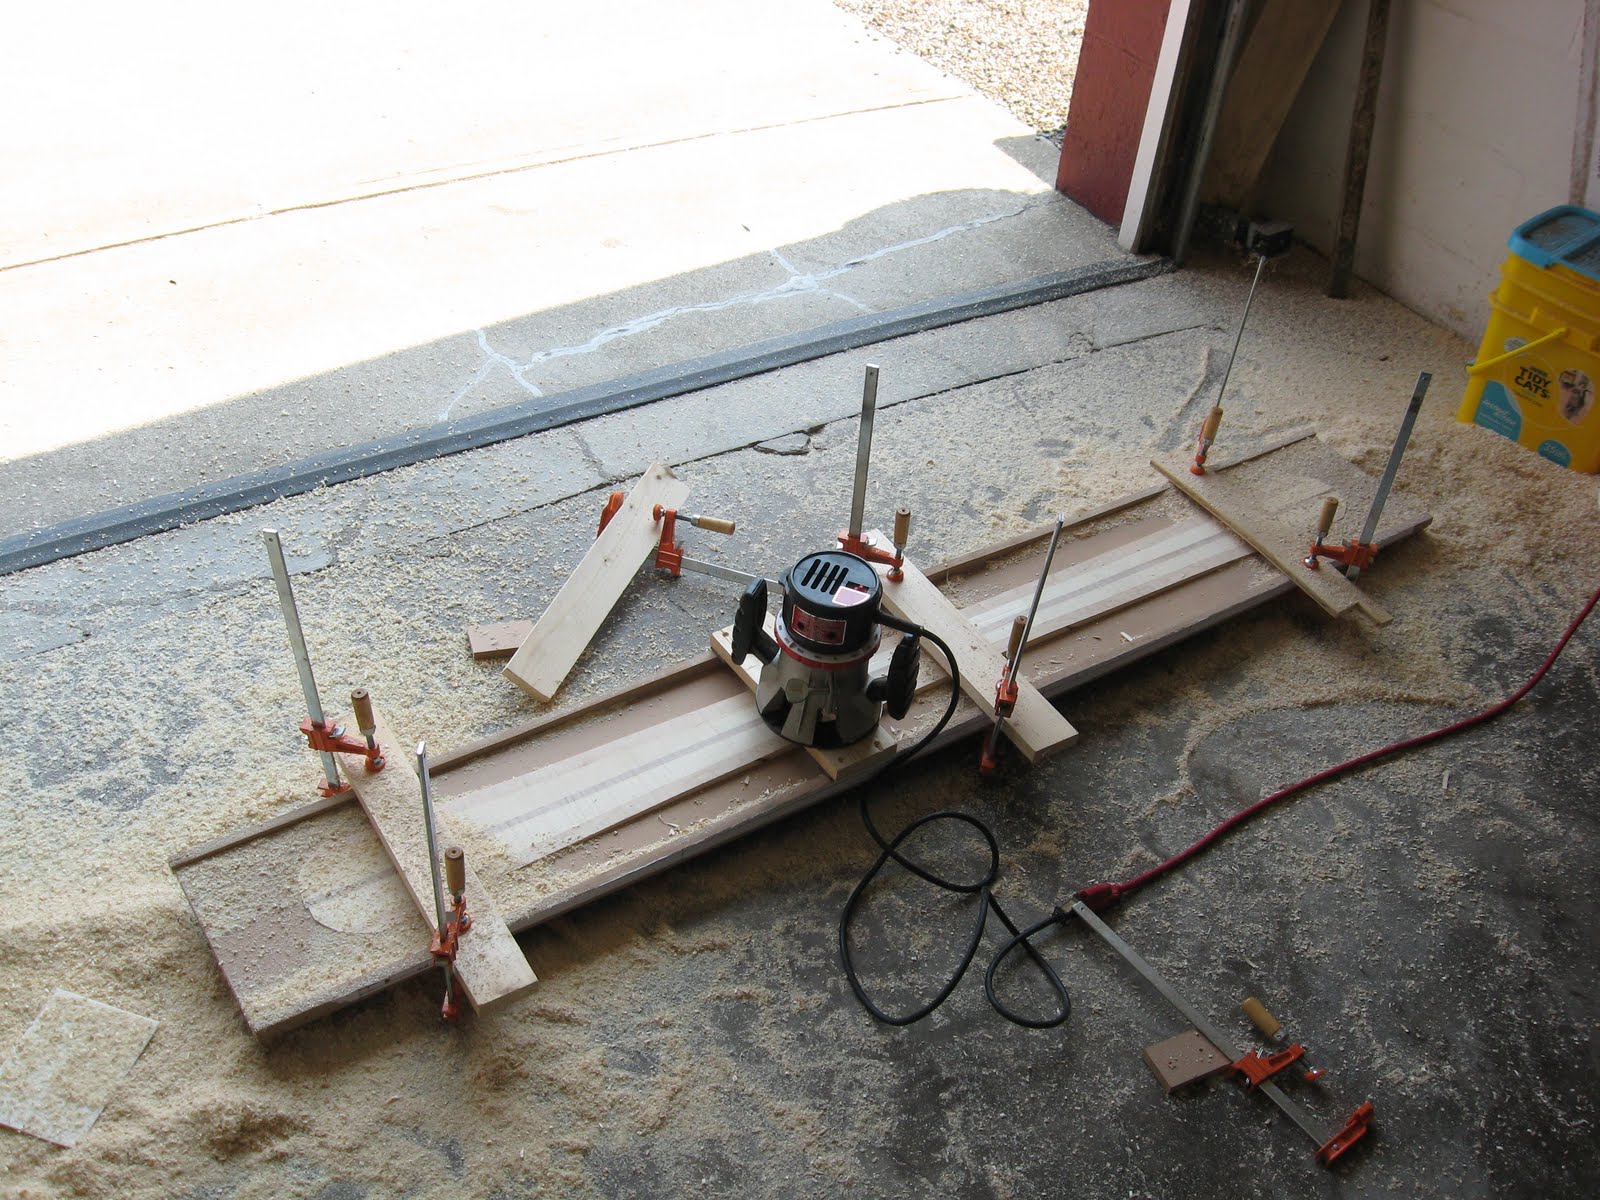
Once planing is complete, the ski thickness must be profiled to size.  A linear profile was chosen for these skis which takes them from 12mm at the boot to 2 mm at the tip and tail.  This is accomplished using the profiling jig that was created earlier.  A router is moved across the ski on a slide which is moved up and down the rail.


 A rapid material removal router bit works best.  It should create a flat cut.


 A slider is used to guide the router along the profiling jig rails.


The following video is played at 12X speed and demonstrates the profiling process.  It takes approximately 20-25 minutes per ski.


The cores are then sanded to remove any unevenness.  Once finished, the cores are ready to be pressed.