Friday, October 14, 2011

Press, Stage One

Depending on the design of your skis and your ability to precisely machine the shape of the ski, pressing the ski can be done in a single stage or in multiple.  The first skis I designed had plastic sidewalls and they were pressed in a single stage. 


Adding a plastic side wall gives the ski a clean look and will protect the core from damage.  They add expense and time to the design as they have to be attached with epoxy to the core.  The plastic used for the sidewall (P-tex) is more dense than wood and has a lower modulus of elasticity (much more flexible) and therefore adds weight to the ski without adding strength.

The cap design is simpler and doesn't require that a plastic sidewall be used.  The core is beveled on the edges and the top sheet is wrapped down over the edge of the the core.  This design reduces the weight of the ski because beveling the core removes material.  Beveling the edges does not compromise the strength of the ski because when the ski is used to make a turn, force is applied at the edge of the ski and is reacted by the boot/binding.  The bending stress across the cross section is smallest at the edge of the ski and increases linear towards the boot mounting point.


The complication that this design adds is that the core must be beveled to allow a cap to be used.  Since I do not have the ability to precisely machine the core to the size of the base, I use a two-stage pressing process.  In the first stage, the base, edges, fiberglass, rubber and core are molded together.  Once pressed, the flashing is trimmed off and the core is beveled precisely using the edge of the ski as a guide. In the second stage the second fiberglass layer, graphics, and top sheet are pressed to the stage one press group.

One of the key steps in pressing the ski is to get the base and the core properly aligned.  In order to do this, I constructed a jig for the mold using ski edging which would precisely align the base and edges.


In order to align the core I glue two pre-drilled blocks of wood to the side of the core at the centerline.  Prior to final layup, I align the core to the base on the mold and drill alignment holes through the predrilled blocks of wood.  Finish nails will be place through the hole in the block of wood on the core and into the holes in the mold for alignment.  A more complex and repeatable method could be designed for this process, but I have low volume production and this method works well.


Once the alignment pieces are attached to the core and a test alignment has been completed, all of the components of the ski need to be staged for layup.  First, a piece of thin plastic is placed on the mold; this is used to prevent extra epoxy from sticking to the mold and ruining it.  The base and edges are then put in place.  The core, fiberglass, and rubber strips are then staged near the mold.  A foam brush is also staged for spreading the epoxy.  The reverse mold, air bladder, and air compressor must also be staged.


Once the components are stage, the expoxy needs to be mixed.  This year I used West System epoxy.  The hardener I chose, 206, is used for a slow cure time.  The usable time is anywhere from 30-45 minutes with this epoxy.  After this time the epoxy starts to harden. At 9-12 hours the epoxy reaches full hardness and reaches full strength by 24 hours.  I always recommend rubber gloves (chemical resistant) and safety glasses.  A well ventilated area is also recommended.


Once the epoxy is mixed it is time to apply it to the ski and place the ski in the press.  The following video is shown at 12X speed and demonstrates this process.


I typically leave the skis in the press for at least 12 hours. Once this time period is passed you can remove the ski from the press.  The ski after pressing looks like the  following:


The following photo illustrates the shape of the ski after molding.  Since the ski is pressed into shape, stress is locked into the wood and will cause the ski to spring back a small amount when it is removed from the mold.  To compensate for this, the mold must exagerate the shape of the ski.  For the Arlia's shown below, the camber on the mold was designed at 30mm expecting a final camber of 15mm.  A measurement after removal from the mold showed a camber of 14mm.


The next step is to trim the flashing (http://en.wikipedia.org/wiki/Molding_flash) from the ski.  This can be done with a band saw, router, or jig saw.  Since my band saw is out of comission this season, I used my jig saw.  In order to save a step I set the jig saw to a 30 degree angle and cut the bevel of the core at the same time.


Trimming the flashing is one of the more difficult processes because it is time consuming and the cutting tool wears out quickly.  The jig saw blade cuts through epoxy, fiberglass, and the wood core;  at the same time the edge of the ski is used as a guide.  All these factors cause the blade to build up heat quickly.  After every six inches of cut, the blade had to be cooled, otherwise it would overheat causing the metal to soften and the teeth to wear more quickly.  A coarse tooth, quick cutting blade is reccomended over a fine tooth blade (clean cutting) as it will cut quicker and last longer.


Once the flashing is trimmed and the bevel is created, a belt sander is used to even out any flaws in the cut and create a rounded edge where the bevel meets the top of the ski.

Once this is complete the ski is ready for stage two pressing.


Wednesday, September 21, 2011

Inverse Mold

The inverse or reverse mold is used to take up space in the ski press so that the bladder is evenly distributed over the ski.  The picture below shows an example of a pressurized ski press with the mold on the bottom, ski and bladder in the middle, and inverse mold on the top.

The inverse mold can be made in any number of ways and does not have to be precise as it does not mold the ski, but takes up space. This year I made my inverse molds from 2x4 lumber.  To start the inverse mold I traced the shape of the mold onto a piece of the lumber.


 The lumber is then cut to length with a chop saw and to shape using a jig saw or band saw and screwed together.


After some finish sanding the inverse mold is ready for use.  To prevent damage to the bladder you can place a cloth in between the bladder and inverse mold, glue cardboard to the underside of the mold, or glue another piece of hardboard to the mold to make it smooth.


Monday, September 5, 2011

Core

The core of the ski is what gives the ski its feel and strength.  Wood is the preferred material for the ski core because of the flexibility, light weight, strength, and snap/feel.  Other materials can be substituted for wood, such as foam or foam rubber and plastic.  Wood and foam are often used together to create the desired core properties.

I prefer a solid wood core; wood is more expensive than foam, but provides for a better feel in my opinion. There are also many varieties of wood that can be mixed to create any feel (maple, poplar, aspen, ash, balsa, etc.). The core is designed with several factors in mind: primarily weight and flexibility (noodle vs barn door feel).  There is a balance here which ski manufactures work hard to achieve.  My first year I used a core made from poplar and aspen; these cores made for a very light ski, but it was also very flexible: the noodle. My second year I used aspen and maple, but also integrated steel and aluminum rods, 3 ft and 5 ft respectively, into the core.  The core was also thicker; this resulted in a ski that was heavy and rigid: the barn door.  These ski both have their place - backcountry/powder vs hard crud.  Last years cores are shown below:

 A 1/8" groove was routed into the side of the core members to place the 3' stainless steel and 5' aluminum rods in the core.


This year I attempted to balance the two by using my knowledge of the past two years.  The core is made from aspen and maple, but is thinner than year two.  I also tried to use some engineering logic to come to a conclusion:


The first step in creating the core is to rough cut the stock material.  This is done using a table saw to rip the boards down their length.  Their width is determined based on the core plans I originally laid out on my templates.


The next step is to cut the curved core members using a pre-fabricated template.  The cores I design use three constant width members and two variable width members.  The constant width members made from maple and run along the edges and in the center of the ski.  The two variable width aspen members are placed in-between the maple members.  I used this design because the constant thickness maple members on the edges create a constant edges pressure.  Also, the core is pretentioned into place.  This pretentioning adds some built-in stress to the ski which will add to edge pressure.  Ski manufacturers will not use this method because it wastes too much material, but I think the properties it gives is worth the loss.  Some of the following pictures will show the members and the pretensioning.  The variable width core members are cut with a jigsaw.

The core members and pretensioning method can be seen in the following pictures:


Using this method, the ski profile does not have to be cut, but is clamped into place. The core members should be sanded to remove any unevenness and ensure that the glue will bond well.


The next step is to clamp and glue the core into place;  I use a standard water resistant wood glue.  Placing a piece of plastic down on your work surface prior to gluing will help to control excess glue.


The core template can then be used to cut the rough tip and tail shape.  This is not the final shape as the core and flashing are trimmed after the ski is pressed.  The template is larger than the final ski by 5mm on every side.


At this point the ski must be planed to size.  The wood used is 3/4" thick which is equivalent to 19 mm.  The ski must be planed to 12 mm; this is the maximum thickness of the ski.  Using the planer is one of my favorite operations because it always works fast and well.


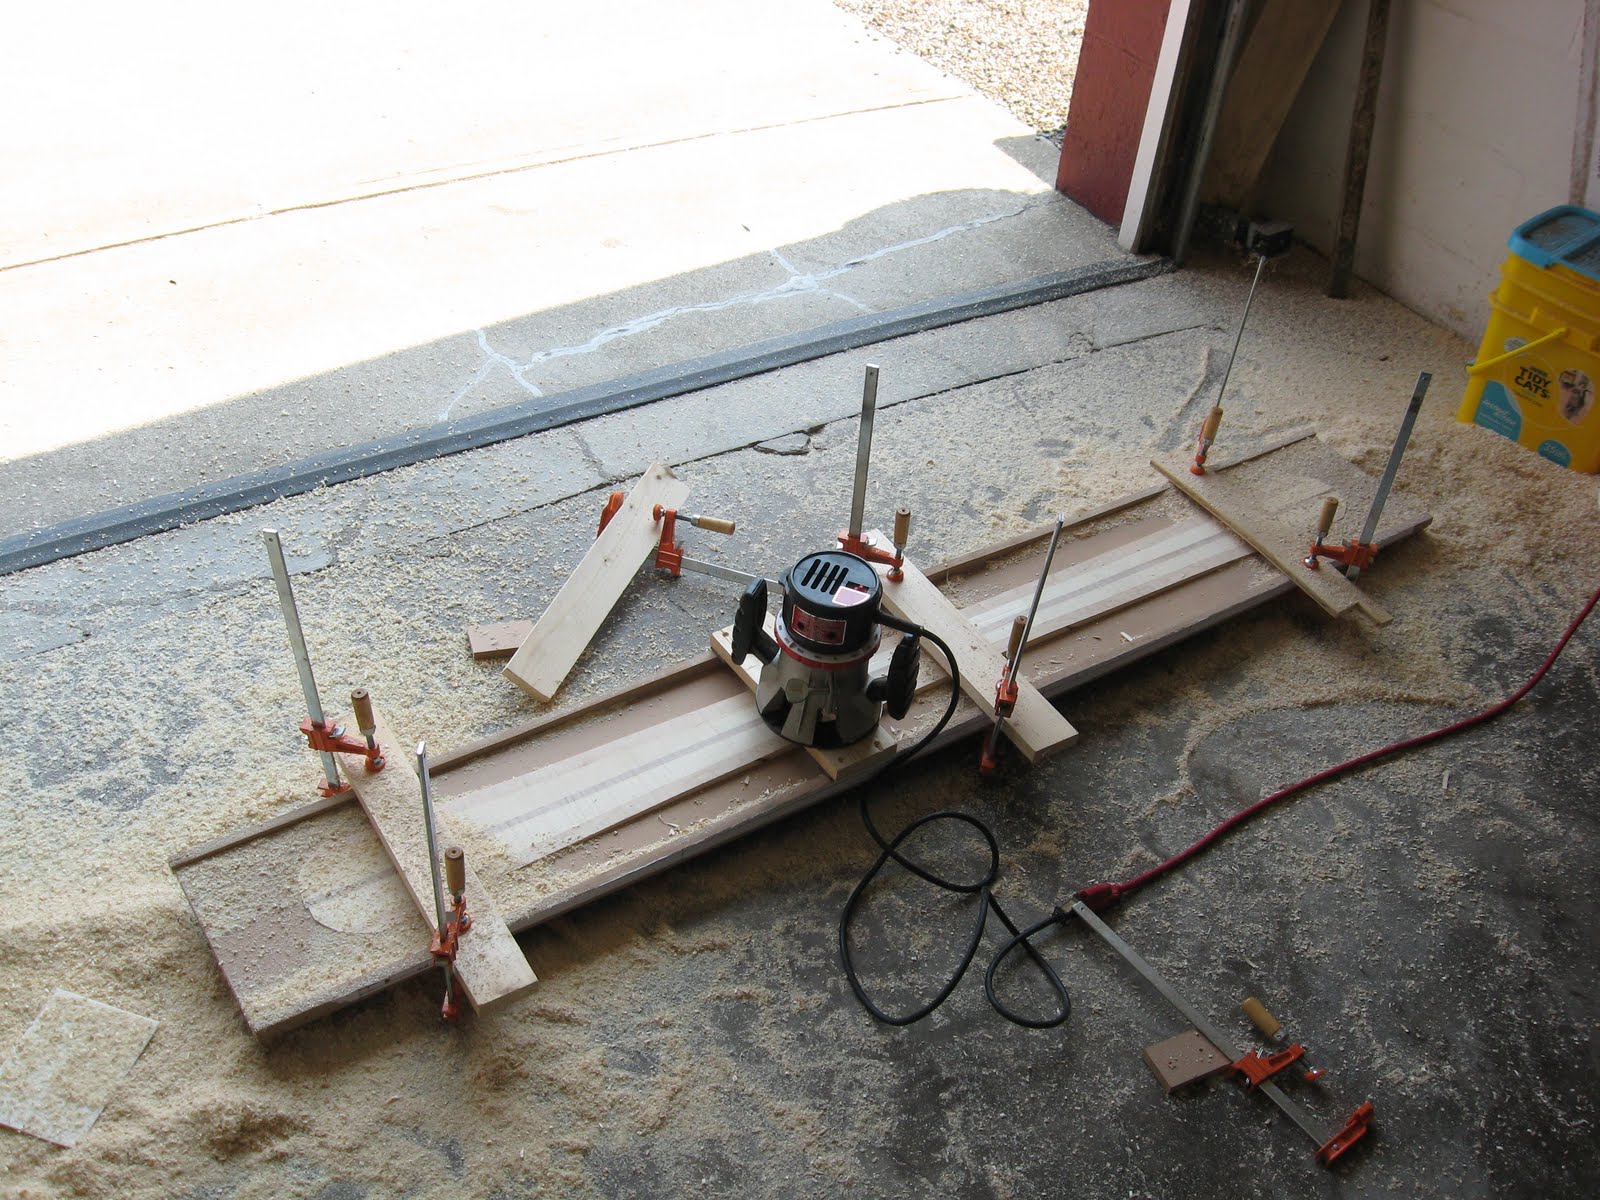
Once planing is complete, the ski thickness must be profiled to size.  A linear profile was chosen for these skis which takes them from 12mm at the boot to 2 mm at the tip and tail.  This is accomplished using the profiling jig that was created earlier.  A router is moved across the ski on a slide which is moved up and down the rail.


 A rapid material removal router bit works best.  It should create a flat cut.


 A slider is used to guide the router along the profiling jig rails.


The following video is played at 12X speed and demonstrates the profiling process.  It takes approximately 20-25 minutes per ski.


The cores are then sanded to remove any unevenness.  Once finished, the cores are ready to be pressed.